

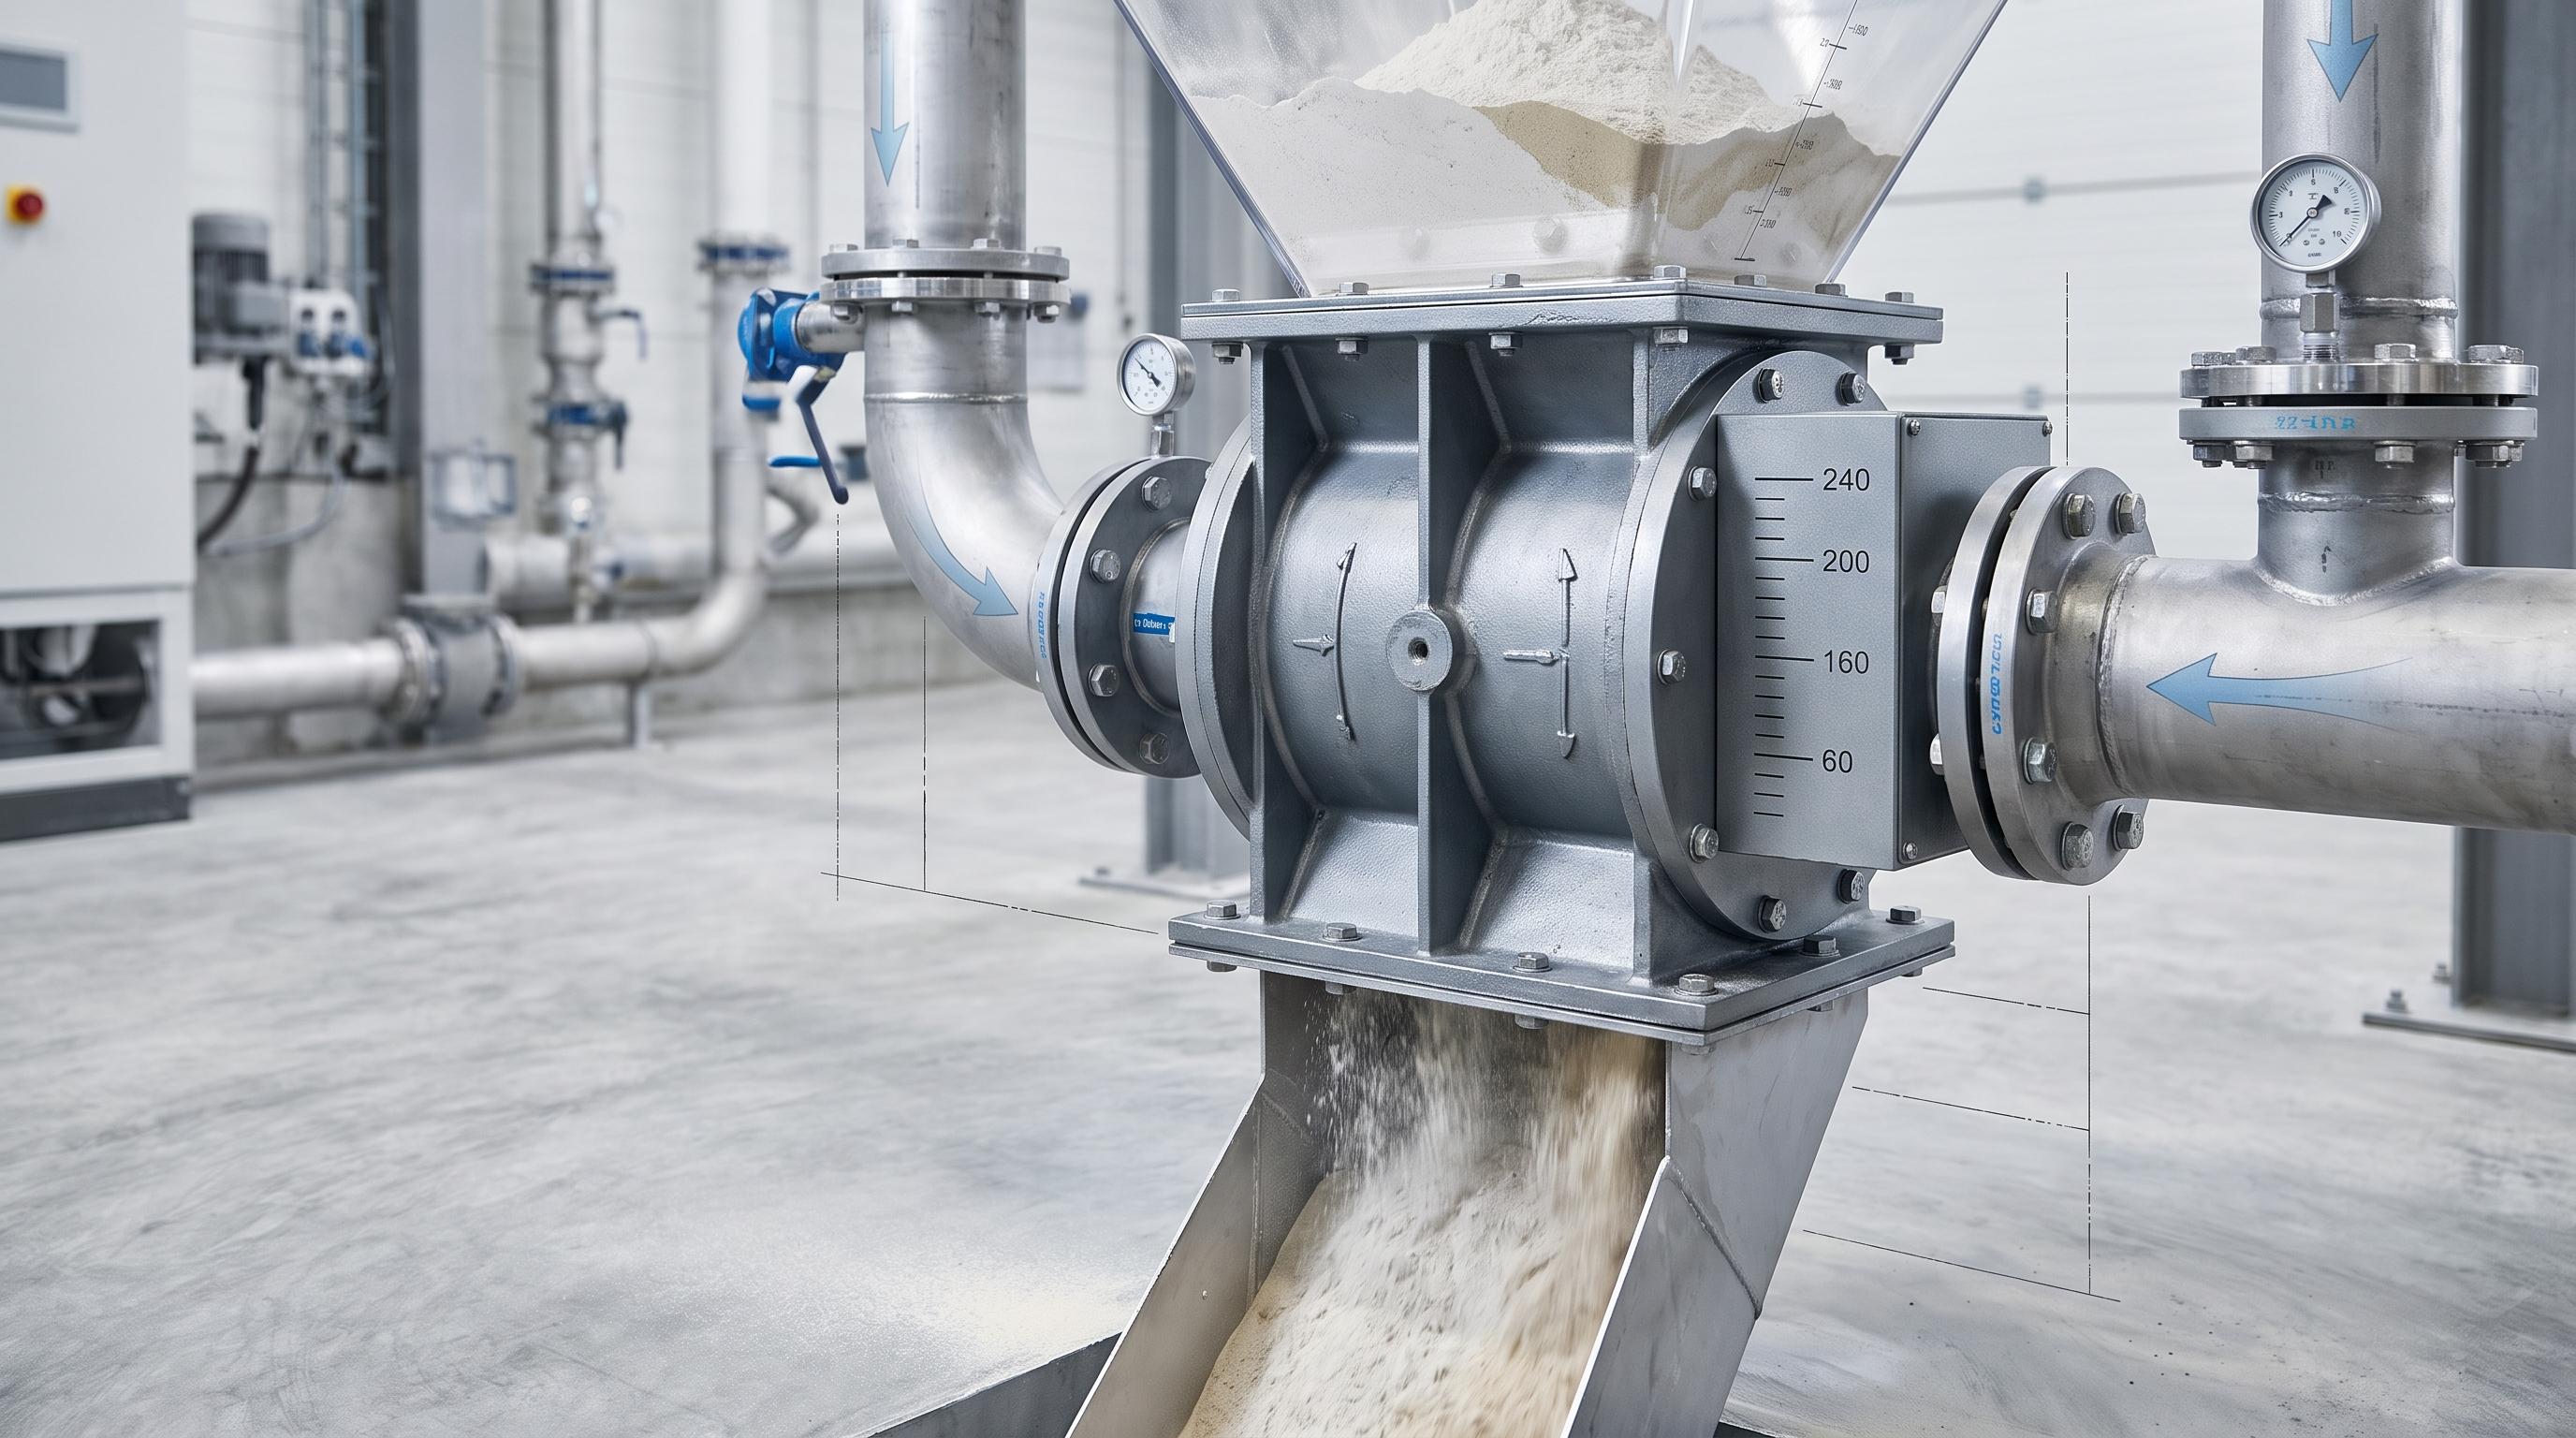
To size a rotary airlock for cement or fly ash, calculate the displacement per revolution you need: feed rate ÷ lightest bulk density ÷ fill factor ÷ (RPM × 60). For cement, start at 80 percent fill. For fly ash, use 65 to 70 percent, and keep the rotor under 25 RPM.
That is the sizing answer most buyers want first. The rest of the job is making sure the number matches the real duty, not the pipe size or a generic chart.
For plant engineers, maintenance teams, and buyers at cement and power plants, this is not a small detail. It sets your throughput, your wear rate, and how often the valve comes back for service.
Sizing comes down to one number: how much material the rotor moves per turn. This guide shows you how to find it.
Displacement needed (ft³/hr) = feed rate (lb/hr) ÷ lightest bulk density (lb/ft³) ÷ fill factor. Divide by revolutions per hour (RPM × 60) to get cubic feet per revolution. Pick the valve that provides it. Use 80 percent fill for aerated cement, 65 to 70 percent for fly ash, and keep the rotor under 25 RPM.
A rotary airlock does two jobs at the same time:
Meters material at a steady rate you set with the rotor speed
Holds back air across the pressure difference between the two sides
Size it on tonnage alone and you get the first job right and the second one wrong. That is the most common sizing miss we see.
Number | What it is | Where to get it |
|---|---|---|
Feed rate | Pounds per hour | Tons per hour × 2,000 |
Bulk density | Pounds per cubic foot | Measure your material, at its lightest |
Fill factor | How full each pocket gets | See the table below |
Rotor speed | RPM | Under 25 |
Get those four and the rest is arithmetic.
Three short steps. In this guide, tons means US short tons, so 1 ton = 2,000 lb.
Step 1. Volume of material you need to move
Material volume (ft³/hr) = Feed rate (lb/hr) ÷ Bulk density (lb/ft³)
Step 2. Rotor displacement that delivers it
Displacement (ft³/hr) = Material volume (ft³/hr) ÷ Fill factor
Step 3. Displacement per turn
Displacement per revolution (ft³/rev) = Displacement (ft³/hr) ÷ (RPM × 60)
Step 3 gives you the number you shop with. From there, compare your required displacement, duty, and operating conditions against our rotary airlock valve range to narrow the right model.
Work in the order above. People often start by picking a size and then work backward to justify it. That is how a valve ends up matched to the pipe instead of the duty.
This is where sizing quietly fails.
Use the lightest weight your material reaches. Not the average. Not the settled weight out of the silo.
Material | Settled | Aerated or loose |
|---|---|---|
Cement dust | ~90 lb/ft³ | ~60 lb/ft³ |
Fly ash | 55 to 75 lb/ft³ | 35 to 50 lb/ft³ |
Size on the settled figure and the valve comes up short the moment the material aerates. Each pocket is now carrying less weight for the same volume.
Measure your own material. A published density table is a starting point.
Cement and fly ash both pull moisture out of the air. Through a Gulf Coast or Southeast summer, humidity stays high for months. Ash sampled in February is not the ash running in August. Give us the worse case.
Pockets never fill all the way. How far short they fall depends on the material.
This is the number that decides whether your valve is right.
Material | Fill factor |
|---|---|
Cement, aerated, gravity feed | 80%, and it can run higher |
Fly ash, light and aerated | 65 to 70% |
Anything feeding a pressure line | 65 to 70% |
Free-flowing powder, general | 80% |
Pellets and dense granules | ~50% |
Three things to know before you use it:
Cement fills high. Aerated cement runs into the pocket almost like a liquid. Size it on a heavy de-rate and you buy a valve bigger than the duty needs. It will not starve your line. It will overfeed it.
Fly ash fills low. It is light and it holds air, so it does not settle cleanly into a turning pocket. Same plant, same rotor, different number.
Fill drops as speed rises. A pocket has less time to load at 40 RPM than at 10. So fill and RPM get decided together.
Keep it under 25 RPM. Run 10 to 20 RPM for the most even feed and the best fill.
Speed costs you twice on cement and fly ash:
Fill drops. Less time to load the pocket, so part of the throughput you thought you gained is not there.
Wear climbs. Abrasive dust drags across the rotor tips every turn.
The rule for abrasive material: upsize the valve and slow it down. A bigger rotor at 15 RPM and a smaller one at 30 RPM move the same tonnage. Only one still seals in two years.
Here is the whole method on a real duty.
The inputs:
Material: cement
Feed rate: 15 tons per hour
Aerated density: 60 lb/ft³ (measured)
Feed: gravity
Target speed: 20 RPM
Feed rate: 15 × 2,000 = 30,000 lb/hr. Material volume: 30,000 ÷ 60 = 500 ft³/hr. Displacement at 80% fill: 500 ÷ 0.80 = 625 ft³/hr. Revolutions per hour: 20 × 60 = 1,200. Displacement per revolution: 625 ÷ 1,200 = 0.52 ft³/rev. Pick the valve that provides at least 0.52 ft³/rev. That lands around a 12-inch valve.
Now check the other end.
If that cement arrives well aerated and the pockets fill closer to full, the same valve at 20 RPM moves about 625 ft³/hr. That is 25 percent more cement than you asked for.
This is why we put speed control on cement duty. You size the valve for the fill you expect. The drive corrects for the fill you get.
Want to run your own numbers instead of a generic chart? Our spec sheet lists cubic feet per revolution for every valve size, so you can go straight from your displacement figure to a model.
Two quick checks before you commit.
Check the speed. If your displacement figure forces the rotor above 25 RPM, go up a size. Do not solve a capacity gap with speed.
Check the inlet. On cyclone and filter duty, the inlet opening sometimes governs instead of the throughput. If the inlet is too small, material bridges above the valve and the rotor runs half empty. The valve is then the wrong size for a reason the math never showed.
Typical valve sizes run from about 6 inches up past 24 inches across the inlet.
Leave yourself margin, but not much. A little headroom is sensible. A lot is not. An oversized valve turns slower than it should, and on fine cement the material has time to pack in the pockets instead of dropping clean. Aim to land inside your speed window rather than two sizes above it.
The math gives you the size. These decide whether it survives cement and ash:
What | What to specify |
|---|---|
Rotor tips | Abrasion-resistant tips in a hard-chrome bore for moderate duty. Stellite hardfacing for harder duty. Ceramic-lined internals with tungsten carbide tips for severe service. |
Rotor style | Closed-end rotor on abrasion-resistant builds, with an air purge on the shroud face so fine powder does not pack there. |
Vanes | Eight is the standard for abrasive service. More vanes seal better and cost a few percent of displacement. |
Tip clearance | 0.003 to 0.005 inches normal. Under 0.0079 inches with two vanes sealing per side if the valve is part of combustible dust isolation. |
Temperature | Give us the real operating temperature, including upsets, so the clearance allows for rotor expansion. |
Location | Tell us if it sits outdoors or in an unheated gallery. |
That last one matters more in the US than people expect. In the Upper Midwest, a cold housing meets warm process gas and sweats. Cement or ash cakes on the damp rotor and bridges the inlet. A valve that ran clean all summer starts plugging on the first hard freeze. Insulating or heat-tracing the inlet is a cheap call now and an expensive one in January.
Clearance is also what sets how much air the valve leaks back up the line. That is a subject of its own, and we cover it on our rotary airlock air leakage page.
The formula does not change. The inputs do.
Aerated cement and raw meal fill high. Size at 80 percent, expect more, and put speed control on it. Abrasion sets the tip package, not the capacity. See our cement plant equipment.
Fly ash is the opposite. Light, air-holding, and it fills low, so use 65 to 70 percent. Ash off the precipitator also runs hot, so clearance has to allow for rotor growth. See our power plant equipment.
Same math, different rating. That dust burns. A valve under a coal or petcoke mill dust collector is usually the part that stops a dust explosion from spreading, so it has to be rated as an isolation device under NFPA 660, not just sized for tonnage.
Sizing off the pipe diameter instead of the calculation
Using the settled bulk density instead of the aerated one
Carrying a fill factor over from a different material
Sizing cement on a pellet de-rate, then overfeeding the line
Solving a capacity shortfall with more RPM
Picking the tip package after the valve is already ordered
Leaving out the operating temperature, then losing the clearance to expansion
Most of the sizing we do for US cement and power plants comes back to two numbers: a density nobody measured at its lightest, and a fill factor carried over from a different material. Both take a minute to check.
Get those right and the valve holds its rate and its seal for years. Get them wrong and no rotor material saves it.
Not sure which size your duty calls for? Send us the material and the tons per hour. We will run the numbers and come back with a size, a speed, and a tip package.
Size on displacement per revolution: feed rate ÷ lightest bulk density ÷ fill factor ÷ revolutions per hour.
Use the lightest aerated density, not the settled weight, and measure it in the humid season.
Cement fills high at 80 percent and up. Fly ash fills low at 65 to 70 percent. Not the same number.
Keep the rotor under 25 RPM. On abrasive duty, upsize and slow down.
Settle the tip package, clearance, and temperature at the same time as the size, not after.
Divide the feed rate in pounds per hour by the material's lightest bulk density. That gives cubic feet per hour of material. Divide by the fill factor for the rotor displacement per hour. Then divide by revolutions per hour, which is RPM times 60, to get cubic feet per revolution. Match that to a valve size.
Use 80 percent on gravity feed, and expect it to run higher. Aerated cement flows into the pocket almost like a liquid. Drop to 65 to 70 percent if the valve feeds a pressure line. Size cement on a heavy de-rate and the valve comes out too big and overfeeds.
No. Fly ash is lighter and holds air, so it fills low. Use 65 to 70 percent for ash against 80 percent for aerated cement. Ash off the precipitator is also hot, so the running clearance has to allow for rotor expansion.
Under 25 RPM. Run 10 to 20 for the most even feed and best fill. Fill drops and tip wear climbs as speed rises, so upsize the valve and run it slower rather than running a small one fast.
Whatever size gives the displacement per revolution your calculation asks for at under 25 RPM. Example: 15 tons per hour of cement at 60 lb per cubic foot and 80 percent fill needs 0.52 cubic feet per revolution at 20 RPM, which is around a 12-inch valve. Do not size off the pipe.
For a first pass, yes. Most calculators do not carry a cement or fly ash option, so they run a generic fill factor. That is the number that decides your size, so check it against your material before you order.
Two signs. If the line runs short with the rotor already near 25 RPM, it is undersized. If you are throttling the drive well below its range to hold the rate, it is oversized. Bridging at the inlet is a third case, and that is usually an inlet or flow problem rather than a size problem.
Delivering advanced conveyor solutions from Houston across the U.S.


